
Grade quotation brief
303 vs 304 Stainless Steel
Quote 303 when a representative machining trial and the service environment support sulfur-assisted chip control in the ordered bar condition. Quote 304 when welding, forming, washdown, product contact or a different product form controls the design. Neither grade can be approved from a generic machinability rating, and a material change requires drawing, corrosion and manufacturing review.
Quote 303 only when machining trials, exposure and the drawing justify a sulfur-bearing free-machining route. Quote 304 when welding, forming, product contact, washdown or broader product-form availability controls the design. Compare dated quotations using the same bar size, tolerances, machining cycle, tool plan, inspection and finish scope; a nominal cutting-speed claim does not establish delivered part cost.
Unsure whether 303 or 304 matches the operating temperature and chemistry? Send the service conditions with the RFQ. We quote the approved designation, product form and test plan.
Request a Quote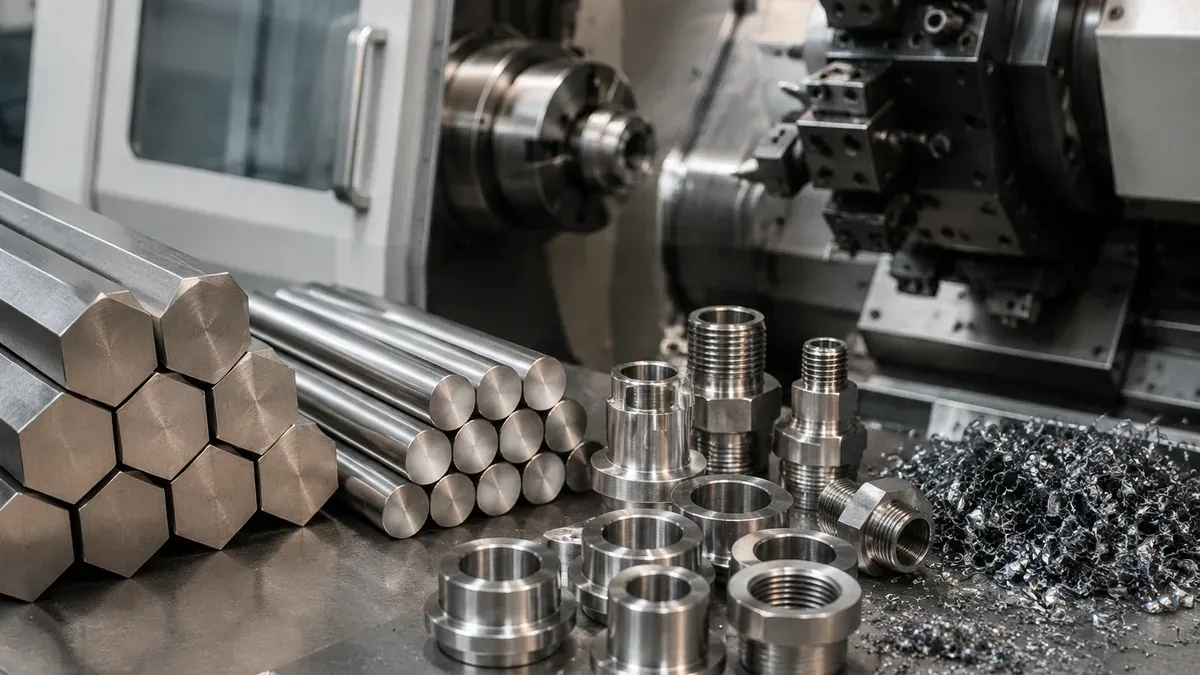
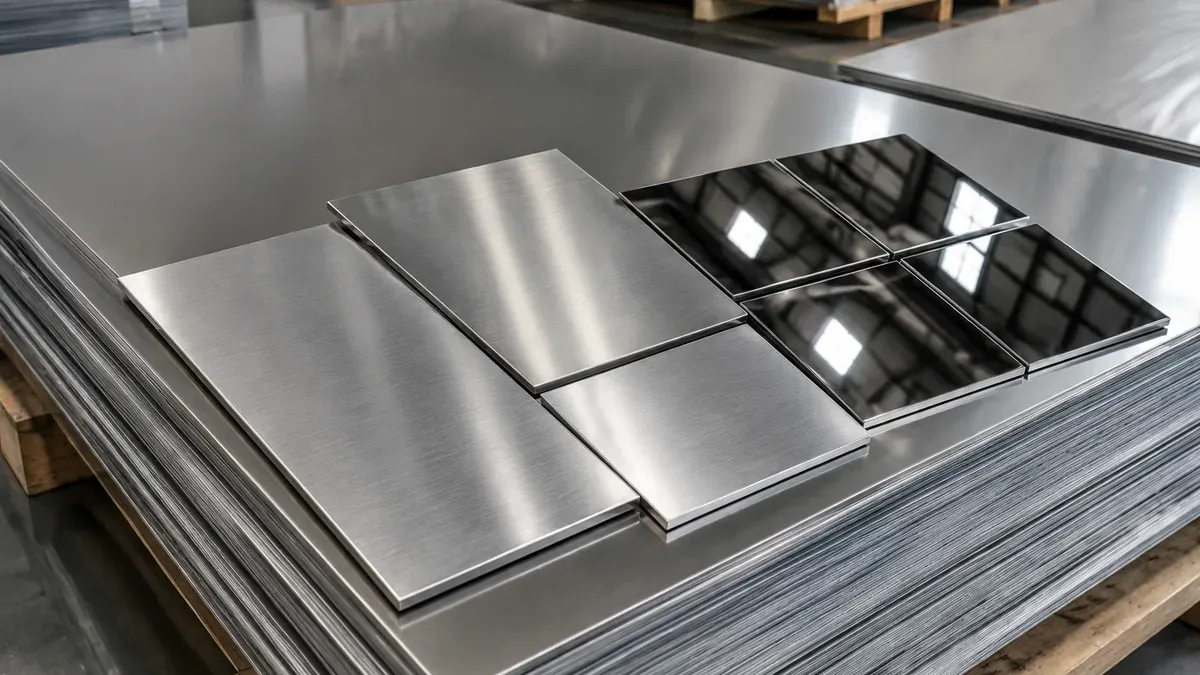
Illustrations identify the compared grade references; they are not photographs of the quoted material or proof of a mill heat.
Decision matrix
Key Differences
Full grade sheets:303 Stainless Steel/304 Stainless Steel
| Factor | 303 | 304 | Procurement decision |
|---|---|---|---|
| Sulfur and inclusions | 303 has a specified sulfur range that promotes chip-breaking inclusions in a free-machining route. | 304 has a lower sulfur limit and follows a general-purpose austenitic fabrication route. | Connect chemistry to trial results, surface requirements and exposure rather than a fixed machining multiplier. |
| Machining behavior | 303 can improve chip control for suitable turned geometry, tooling, coolant and bar condition. | 304 work hardening and chip behavior require a different tool, feed, speed and process plan. | Quote the validated cycle, tool life and rejection criteria for the actual part and machine. |
| Joining and forming | 303 is not an automatic choice for welded or heavily formed assemblies because its sulfur route changes fabrication behavior. | 304 supports established welding, bending and drawing practices when procedures and surface restoration are controlled. | Use 304 for an approved welded or formed route unless a specialist procedure explicitly qualifies 303. |
| Corrosion and finish | 303 inclusions can narrow corrosion and surface-cleanability margin in wet or aggressive exposure. | 304 generally supports a broader wet-service and finish basis, but chlorides and crevices still require review. | Define exposure, cleaning, roughness, passivation and acceptance tests before choosing the material. |
Service and production route
Corrosion and Fabrication Boundaries
303 corrosion screening
- For this 303 vs 304 review, General corrosion resistance comes from the chromium-rich passive film; nickel, molybdenum, nitrogen and copper change performance by grade.
- For this 303 vs 304 review, Check chlorides, temperature, crevices, deposits, process chemistry and cleaning conditions. A grade designation alone is not a service-life guarantee.
304 corrosion screening
- For this 303 vs 304 review, 304 relies on a chromium-rich passive film for general atmospheric, indoor and many process duties, but it is not automatically suitable for warm chloride, coastal salt deposits or persistent crevice-prone service — 316/316L or a higher alloy may be needed.
- For this 303 vs 304 review, Against lower-nickel 201, annealed 304 usually offers more corrosion margin in humidity, outdoor wetting and chemically cleaned food-contact duty; against ferritic 430 it remains the more formable, weldable austenitic default when magnetism and deep drawing matter.
- For this 303 vs 304 review, Review chlorides, temperature, pH, deposits, crevices, drainage, cleaning chemistry, weld heat tint and surface finish for the actual component. A grade designation alone is not a service-life guarantee.
| Operation | 303 | 304 |
|---|---|---|
| Welding | Generally weldable with a qualified procedure and matching or over-alloyed filler where required; remove heat tint when corrosion service demands it. | Generally weldable with a qualified austenitic procedure, matching or over-alloyed filler where required, controlled heat input and heat-tint removal when corrosion service demands it. For as-welded heavy sections, prefer 304L or dual-certified material meeting the low-carbon limit rather than assuming standard 304 HAZ behavior. |
| Forming | Good ductility is typical, but rapid work hardening increases forming load and springback; bend radius and intermediate annealing depend on grade and reduction. | Annealed 304 sheet and strip draw and bend well, but the alloy work-hardens during forming — tooling load, springback, bend direction, draw ratio and any intermediate anneal must be proven on the actual gauge and reduction route. |
| Machining | Use rigid tooling, positive feeds and controlled heat because the material work-hardens; free-machining grades require separate corrosion and welding review. | Use rigid tooling, positive feeds and controlled cutting heat to avoid a work-hardened surface; qualify the route on the delivered condition. Free-machining sulfur grades (for example 303) require separate corrosion and welding review. |
| Heat treatment | Solution annealing and rapid cooling restore the intended condition where applicable. Austenitic grades are not hardened by conventional quench-and-temper treatment. | Solution annealing with rapid cooling restores the intended annealed austenitic condition after suitable cold work or fabrication where applicable. Conventional quench-and-temper treatment does not through-harden austenitic 304. |
Reference data
Composition and Mechanical Requirements
Values below come from each grade's displayed reference dataset. Product form, thickness, condition and contracted standard can change the applicable acceptance table.
Chemical composition (wt%)
| Element | 303 | 304 |
|---|---|---|
| C | ≤0.15 | ≤0.08 |
| Mn | ≤2.00 | ≤2.00 |
| Si | ≤1.00 | ≤0.75 |
| Cr | 17.0–19.0 | 17.5–19.5 |
| Ni | 8.0–10.0 | 8.0–10.5 |
| P | ≤0.20 | ≤0.045 |
| S | ≥0.15 | ≤0.030 |
| Mo | ≤0.60 (optional) | - |
| N | - | ≤0.10 |
Mechanical properties
| Property | 303 | 304 |
|---|---|---|
| Tensile strength (annealed, typical) | ≈620 MPa | - |
| Yield strength (0.2%, typical) | ≈240 MPa | - |
| Elongation (50 mm, typical) | ≈50% | - |
| Hardness | ≤262 HBW | ≤201 HBW |
| Tensile strength | - | ≥515 MPa (75 ksi) |
| Yield strength (0.2%) | - | ≥205 MPa (30 ksi) |
| Elongation (50 mm) | - | ≥40% |
Quotation workflow
Application Decisions
- For high-volume turned parts, provide machine type, bar feeder, tool system, coolant, operations, cycle target, tolerance, roughness and deburring plan.
- For valve or instrument components, document process fluid, cleaning, pressure, wear, threads, sealing surfaces, PMI and leakage requirements.
- For welded or formed assemblies, use the approved 304 route unless a formal qualification covers 303 joining, cracking risk and final properties.
- For food, pharmaceutical or washdown parts, define product-contact rules, finish, crevices, passivation and cleaning chemistry before material approval.
Quote 303 when
- Turned bushings, fittings and fastener parts whose drawing and exposure accept 303
- CNC or automatic-lathe programs where chip control is validated on the ordered bar condition
- Dry or lubricated mechanical components with documented corrosion and cleaning limits
- Orders that can source the exact 303 bar size, tolerance, straightness and traceability package
Quote 304 when
- Welded, bent or deep-formed assemblies qualified around an S30400 route
- Washdown, outdoor or product-contact parts whose corrosion basis accepts 304
- Sheet, tube or fabricated forms not covered by the proposed 303 supply route
- Parts needing finish, passivation and cleanability controls supported by 304 fabrication
Hold point
Do Not Substitute Without Review
- Do not replace 304 with 303, or 303 with 304, without drawing approval and review of machining, welding, forming, corrosion and finish requirements.
- Do not convert a handbook machinability index or supplier cutting-speed example into a guaranteed cycle-time or tool-life outcome.
- Do not approve 303 for product contact, washdown or chloride exposure from its austenitic family name.
- Do not use flat-product 304 properties as acceptance values for 303 bar or transfer bar data across sizes and conditions.
Specification boundary
Standards, Temperature and Approval
Product and project approval
ASTM A582 can govern specified free-machining stainless bar, while ASTM A276 or A479 can govern other bar contexts and ASTM A240/A240M can govern 304 flat product. The current contract edition, exact UNS designation, size, condition, drawing, equipment rules and authorized material reviewer control acceptance.
Temperature boundary
This page sets no universal operating-temperature range for 303 or 304. Temperature changes corrosion, lubricant, cleaning and mechanical requirements, while cold work, product condition, section, load and any joining thermal cycle change the relevant properties. The drawing and governing code control approval.
Commercial comparison
Cost and Availability Factors
Quote 303 and 304 on one RFQ with the same product form, dimensions, tests and documents. This page does not represent current stock, price or lead time.
Cost factors
- Current bar availability, diameter, tolerance, straightness, condition, quantity and delivery window.
- Validated cutting parameters, tool consumption, machine time, chip handling, deburring and inspection cycle.
- Material yield, cutoff allowance, rejection risk, surface finishing, passivation and cleaning scope.
- MTC, PMI, dimensional report, packing, freight, Incoterm and drawing-change approval.
Inputs for a like-for-like quotation
- UNS S30300 or S30400, product form, material and dimensional standards, drawing revision and substitution policy.
- Bar or part dimensions, tolerances, straightness, quantity, condition, surface finish, roughness and edge requirements.
- Machine and tooling route, operations, thread or bore details, coolant limits, cycle assumptions and inspection plan.
- Service fluid, temperature, chlorides, cleaning, washdown, lubrication, product contact and corrosion acceptance.
- MTC, heat traceability, PMI, dimensional or surface reports, packing, destination, Incoterm and schedule.
Continue the specification
Related Grades, Standards and Applications
Grade references
Applications
303 Stainless Steel Hex Bar
303 free-machining stainless steel hex bar in cold-drawn condition for turned and milled fittings, fasteners and components where machining productivity is the priority.
View details →
304 Stainless Steel Sheet
304/304L ASTM A240 sheet in 2B, BA, No.4 and mirror. Common inquiry range 0.3–6.0 mm, 1000/1219/1500 mm widths, cut to size with quoted documents.
View details →
304 Stainless Steel Welded Pipe
304 welded stainless steel pipe and tube to ASTM A312, A249 and A554 — industrial, sanitary and polished decorative, round, square and rectangular sections.
View details →
304 Stainless Steel Round Bar
304/304L round bar in bright, peeled or hot-finished routes. Common inquiry range 3–300 mm diameter, 3 m / 6 m or cut-to-length, for pins, shafts and fittings.
View details →
Buyer questions
Frequently Asked Questions
Are 303 and 304 the same strength?
Their displayed room-temperature minimums depend on product standard, form, size and condition and should not be treated as identical design values. Use the certificate and governing specification for the ordered 303 bar or 304 product.
How much faster does 303 machine than 304?
No universal multiplier applies. Machine power, bar condition, tool material, geometry, coolant, depth of cut, finish, tolerance and chip handling all affect cycle time and tool life. Run a representative machining trial before quoting production output.
Is 303 acceptable for food-contact parts?
Acceptance belongs to the equipment specification and applicable hygiene rules. Sulfide inclusions, surface finish, crevices and cleaning chemistry require review; do not substitute 303 for an approved 304 or 316L product-contact drawing without authorization.
Published by Tsingshan (Shandong) Iron & Steel Co., Ltd..Sources, update policy and technical limitations.
Quote request
Get a Stainless Steel Quote
Send the product, grade and quantity you already have. We will complete the specification and quote the supply route.