
Surface procurement brief
Electropolished Stainless Steel Finish
Use electropolishing when controlled electrochemical material removal is required to reduce microscopic peaks, produce a bright directionless surface, or support a specified cleaning regime on suitable stainless geometry. The process follows the incoming material, weld profile, inclusions, scratches, and current roughness; it cannot fill pits, close crevices, repair a poor joint, or reach every shielded surface equally. The order should define alloy, completed-fabrication condition, mechanical prefinish, removal allowance, masked features, internal and external coverage, roughness method, visual limits, cleaning, passivation or final treatment, records, closures, and packing.
- Use this guide for
- Functional surface-removal and cleanability specification for fabricated stainless equipment
- Relevant to
- Pharmaceutical, biotechnology, high-purity, sanitary tube, food-equipment, and precision-fabrication buyers
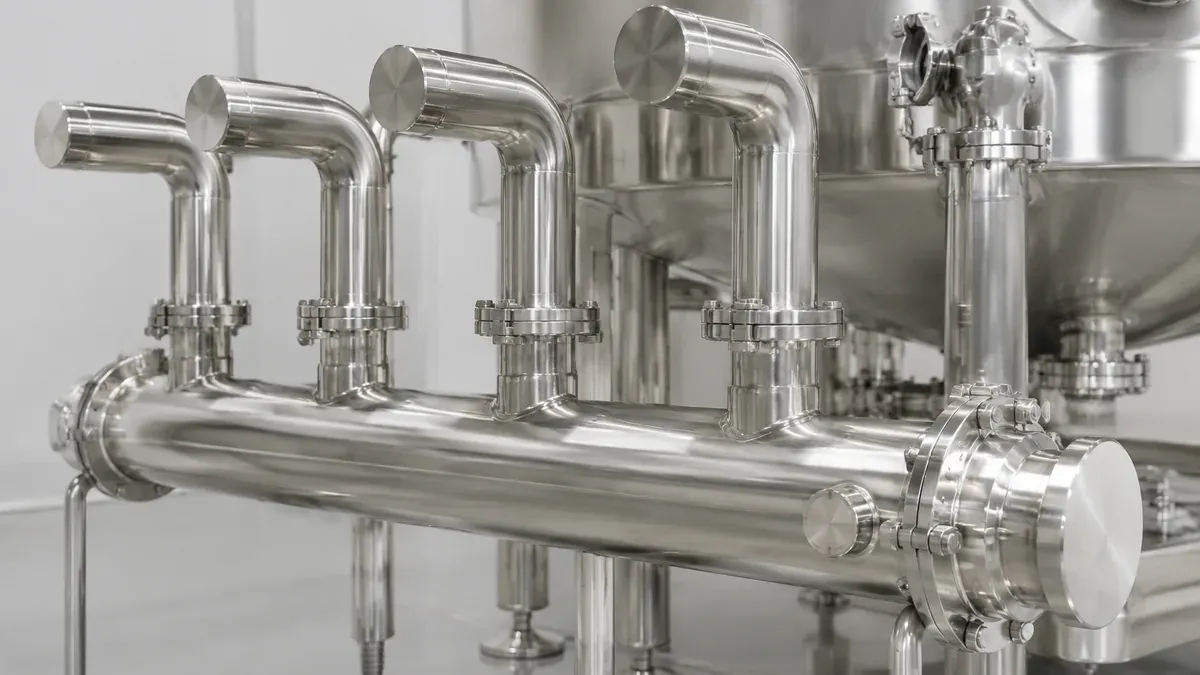
Incoming surface to delivered finish
Finish Class and Process Route
Finish class
Anodic electrochemical surface-removal process applied under controlled chemistry and electrical conditions to a prepared stainless component.
Incoming-surface dependency
Base-metal cleanliness, inclusions, free-machining constituents, mill or abrasive finish, weld penetration and blending, scratches, pits, burrs, and geometry govern the result. Electropolishing preferentially removes peaks but does not create acceptable macro-geometry from an unsuitable starting surface.
| Stage | Control to state | Risk if omitted |
|---|---|---|
| Material and prefinish qualification | Confirm alloy, heat condition, weld route, starting roughness, defect allowance, mechanical prefinish, dimensions, and material-removal budget. | Different alloys, weld zones, inclusions, or starting textures may remove at different rates and reveal pits or color variation. |
| Cleaning, masking, and fixturing | Degrease completely, mask threads and dimensional features, define electrical contact points, and fixture for solution flow and drainage. | Residual oil, weak contact, gas pockets, poor drainage, or mask leakage can produce incomplete or unwanted removal. |
| Controlled electropolishing | Use the qualified provider procedure and define coverage, current-distribution controls, removal range, agitation or circulation, and internal access. | Shielding and current concentration can cause dull zones, edge attack, uneven gloss, or excessive removal at projections. |
| Rinse, neutralize, clean, and verify | Specify final rinse quality, neutralization, drying, visual and roughness inspection, contamination control, documentation, and closures. | Retained electrolyte, dirty rinse, incomplete drying, or unclean handling can compromise the accepted surface before use. |
Measurable and visual controls
Acceptance Criteria
| Criterion | What to specify | Boundary |
|---|---|---|
| Starting and final roughness | State measurement parameter, instrument, cutoff, direction, locations, sampling, prefinish, and final limit where roughness is functional. | A maximum Ra does not describe pits, inclusions, waviness, weld contour, or complete geometry access. |
| Material removal and dimensions | Define nominal or allowable removal, remaining wall or feature dimensions, masked surfaces, and post-process dimensional checks. | Electropolishing removes metal and can affect threads, edges, thin walls, sealing faces, and toleranced features. |
| Coverage and visual condition | Map internal and external surfaces, welds, contact points, shielded zones, expected brightness, pits, stains, streaks, and non-uniform areas. | Brightness alone does not demonstrate roughness, cleanliness, or complete treatment. |
| Cleanliness and final treatment | Define rinse-water quality, residue limits, passivation or cleaning step, dryness, handling class, and project-approved verification. | The electrochemical process does not automatically validate the complete equipment cleaning or hygiene program. |
| Records and traceability | Require procedure revision, item identity, starting condition, run data, inspection results, deviations, and closure status as appropriate. | A generic certificate without item and scope traceability cannot establish that all specified surfaces were processed. |
Preserve the ordered surface
Fabrication, Cleaning, Film, and Packing
| Stage | Effect on finish | Required control |
|---|---|---|
| Welding and mechanical finishing | Uneven weld crowns, undercut, pores, coarse grinding, and heat tint remain influential after material removal. | Complete and inspect the qualified weld and prefinish route before electropolishing, including representative internal joints. |
| Threads, seals, edges, and thin walls | Current density and solution access can remove excess material from projections or leak beneath masks. | Identify critical dimensions, qualify masking and fixturing, and measure listed features after processing. |
| Internal tube and vessel surfaces | Long runs, branches, dead legs, fixtures, gas, and current distribution can cause unequal treatment. | Define electrode arrangement, circulation, venting, drainage, coverage verification, and inaccessible-area disposition. |
| Assembly, cleaning, and shipping | Later welding, dirty assembly, fingerprints, residues, and unclean caps can invalidate the accepted final state. | Sequence electropolishing after major hot work, control clean assembly, use compatible closures, and pack to the specified cleanliness level. |
Finish-specific disputes
Defects, Causes, and Prevention
| Defect | Likely cause | Prevention input |
|---|---|---|
| Uneven gloss or dull shielded zones | Current distribution, gas masking, poor contact, geometry, solution flow, or inconsistent starting surface changes removal. | Qualify electrodes and fixtures on representative geometry, map coverage, and inspect critical internal and external areas. |
| Pits revealed after processing | Base-metal inclusions, weld porosity, embedded contamination, or deep abrasive damage may become visible as surrounding metal is removed. | Set incoming-material and weld limits, inspect after prefinish, and agree repair or rejection rules before the final process. |
| Excessive edge or feature removal | High current density at projections, mask failure, long exposure, or thin geometry can change dimensions. | Control the qualified removal window, mask critical areas, use witness pieces where appropriate, and perform post-process dimensional checks. |
| Residue or staining after rinse | Retained electrolyte, inadequate neutralization, contaminated rinse water, poor drainage, or drying marks can remain on the surface. | Validate rinse and drainage, define final-water and residue acceptance, dry completely, and protect the item immediately. |
Application-led choice
Where This Finish Fits
| Use case | Selection guidance | Approval boundary |
|---|---|---|
| Pharmaceutical and high-purity vessels or piping | Combine electropolishing with specified alloy, weld quality, internal geometry, maximum roughness, cleaning, inspection, traceability, and system validation. | The finish by itself does not create hygienic design, sterile condition, or project acceptance. |
| Sanitary tube and fittings | State whether loose components or completed weldments are processed, which bore surfaces are covered, measurement locations, closures, and handling class. | Coupon results do not prove uniform treatment through every bore, branch, or field weld. |
| Decorative bright components | Use an approved visual sample and control substrate, geometry, contact points, handling, and film where brightness is the main requirement. | Select mirror polishing instead if reflected-image character rather than electrochemical smoothing is the primary goal. |
Copy structure, replace values
Purchase Description Example
Continue the specification
Products, Grades, Standards, and Applications
Product forms
Product and finish standards
Application briefs
Buyer questions
Frequently Asked Questions
Can electropolishing remove deep scratches or poor weld geometry?
No. It preferentially removes microscopic peaks but follows the existing macro-surface. Deep scratches, pits, undercut, crevices, porosity, and poor weld contour require qualified mechanical or fabrication correction first.
Does a bright electropolished surface prove the required roughness?
No. Brightness is visual. Functional roughness needs a specified parameter, instrument, cutoff, direction, locations, sampling plan, and acceptance limit on the actual geometry.
Is electropolished stainless automatically suitable for pharmaceutical service?
No. Suitability depends on alloy, hygienic design, weld quality, roughness, cleaning, drainage, documentation, validation, and project rules. Electropolishing is one controlled surface process within that system.
Published by Tsingshan (Shandong) Iron & Steel Co., Ltd..Sources, update policy and technical limitations.
Quotation package
What to Include in the RFQ
- Material standard, edition, grade, heat condition, dimensions, wall, and item traceability
- Completed fabrication, weld profile, starting finish, mechanical prefinish, and defect allowance
- Internal and external coverage, exclusions, electrical contact points, masks, and inaccessible geometry
- Removal allowance, remaining dimensions, edges, threads, seals, tolerances, and post-process checks
- Starting and final roughness parameter, instrument, cutoff, direction, locations, and sampling
- Visual, pit, cleanliness, rinse, passivation, residue, dryness, record, and witness requirements
- Clean handling, caps, bags, separators, packing, destination, and quantity
Quote request
Get a Stainless Steel Quote
Send the product, grade and quantity you already have. We will complete the specification and quote the supply route.